


Blog
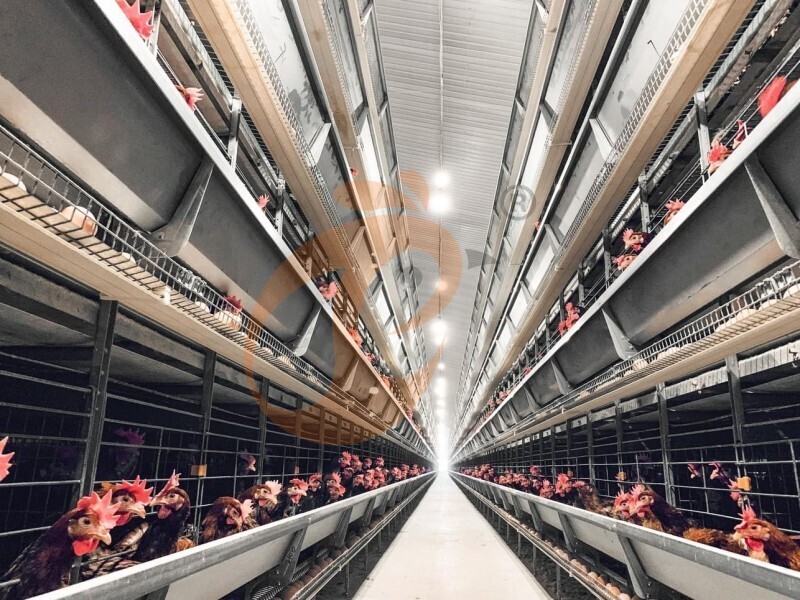
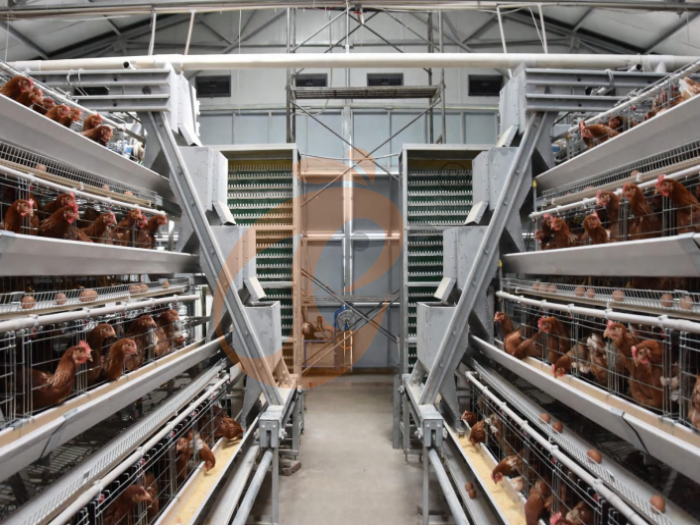
Floor rearing system equipment boosts layer flock production performance across commercial layer housing facilities worldwide.
Sensors maintain optimal litter moisture under 20% to prevent disease transmission while protecting layer floor equipment.
Precision feeding lines deliver 110 grams of feed daily to maintain flock weight uniformity above 95%.
Climate automation regulates ventilation rates up to 7 m³/hr per kilogram for peak layer health.
Investing in high-grade layer floor management machinery ensures long-term operational efficiency and sustainable profits.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, +2348111199996, or click to learn more.
Engineering Specifications And Spatial Parameters
Layer floor rearing system design demands heavy-duty floor layer farming equipment built to rigorous zootechnical structural metrics.
Concrete base foundations require 150 mm thickness alongside high-density floor layer house equipment membranes.
Perimeter steel sidewalls feature 1.2-meter knee structures supporting commercial layer floor management equipment frames.
Support posts withstand 35 mpa compressive force to hold automatic layer rearing system overhead assemblies securely.
Technical Parameters For Floor Housing Infrastructure
Data is for reference only.Swipe horizontally to view full table.
Optimizing Litter Management And Bedding Protocols
Tip 1: Initial Depth Control
Floor layer management equipment performance relies on spreading 8.5 cm deep kiln-dried bedding across deep litter floor layer equipment systems.
Continuous layer floor housing equipment operations require wood shaving particles sized strictly at 3.2 mm.
Tip 2: Moisture Mitigation
Mechanized floor rearing system scarifiers must turn surface litter every 72 hours at 120 rpm.
Automatic layer floor equipment agitation minimizes surface crusting while optimizing floor rearing layer equipment airflow.
Tip 3: pH Stabilization
Spreading 0.45 kg per square meter of agricultural gypsum preserves floor layer system sanitation levels.
Controlling ammonia release extends layer house floor equipment durability whenever moisture readings cross 21.5%.
Tip 4: Replenishment Cadence
Adding 0.12 metric tons of fresh bedding per 100 square meters weekly stabilizes layer floor housing conditions.
Sustained poultry floor layer equipment hygiene safeguards bird welfare and maintains high egg laying production efficiency.
Feed Distribution And Nutrient Delivery Specifications
Data is for reference only.
Swipe horizontally to view full table.
Automated Climate Control And Ventilation Architecture
Air Intake Phase
Floor rearing system motorized louvers open 450 mm at 12 mm/sec actuator speed.
Layer floor equipment pressure sensors calibrate static levels to 25 pa.
Automated layer house equipment delivers fresh air volumes at 4.5 m³/hr per kilogram live weight.
Thermal Mixing Phase
Floor layer house equipment circulation fans measuring 1.5 m spin at 320 rpm.
Layer floor housing equipment heaters generate 75 kw output using 6.2 kg/hr propane.
Commercial floor layer equipment regulators maintain relative humidity between 55.0% and 65.0%.
Exhaust Extraction Phase
Layer rearing floor equipment tunnel fans measuring 1.25 m evacuate 42,000 m³/hr.
Automatic floor layer equipment controllers stabilize negative pressure differential at 38 pa.
Floor layer farming equipment exhausts 100% of internal barn air every 180 seconds completely.
Drinking Systems And Hydration Infrastructure Data
Data is for reference only.
Swipe horizontally to view full table.
Comprehensive Equipment Package Recommendation
Selecting a complete floor rearing system setup ensures full compatibility across all automated layer floor equipment components.
Chain drive feeding lines transport 1,500 kg/hr using 2.2 kw electric drives in commercial floor layer equipment facilities.
High-flow layer house floor equipment nipple lines deliver continuous fresh water under 0.2 mpa operational water pressure.
Centralized layer floor management equipment controllers regulate exhaust fans operating at 30 pa static pressure efficiently.
Egg Collection And Nesting Box Architecture Specifications
Data is for reference only.Swipe horizontally to view full table.
Biosecurity And Sanitization Protocols
Disinfecting floor rearing system housing prevents disease outbreaks and maintains layer floor equipment hygiene standards.
Entryways incorporate automated boot sprayers delivering sanitizing chemical sprays at 1.5 mpa through floor layer house equipment passages.
External vehicle wash portals treat incoming delivery trucks using 18.0 l/min high-pressure floor layer farming equipment pumps.
Saturated steam generators operating at 115 °c and 2.0 mpa thoroughly sterilize layer floor management equipment surfaces.
Lighting Systems And Photoperiodic Control Data
Data is for reference only.
Swipe horizontally to view full table.
Waste Removal And Manure Management Machinery
Scraper Blade Activation
Floor rearing system hydraulic units engage at 14.0 mpa driving blades at 0.15 m/sec.
Automated layer floor equipment scrapers sweep 2.5 m concrete channels using 8.0 mm steel plates.
High-capacity layer floor housing equipment clears 450 mm manure trenches effectively.
Cross-Conveyor Transfer
Commercial floor layer equipment paddle elevators run 600 mm belts powered by 3.0 kw motors.
Layer house floor equipment conveyors elevate organic waste along a 22.0-degree incline at 0.5 m/sec.
Precision layer floor management equipment hoppers receive 1.5 metric tons per batch.
External Storage Management
Automatic layer rearing system augers measuring 200 mm rotate at 60 rpm.
Specialized floor layer farming equipment drying tunnels pump 1,200 m³/hr heated air at 35.0 °c.
Industrial floor layer equipment transfer units store waste under 25.0% moisture limits safely.
Economic Return On Investment And Performance Metrics For Commercial Operations
European union standard reference only.
Data is for reference only.
Swipe horizontally to view full table.
Frequently Asked Questions
Q1: How does automated floor rearing system machinery improve layer flock egg production?
A1: Automated floor rearing systems optimize feed conversion rates while maintaining 0.22 mpa water pressure and precise lighting schedules, boosting egg output by up to 6.2% per batch.
Q2: What floor rearing system ventilation rate keeps litter moisture below critical levels?
A2: Operating tunnel fans at a rate of 6.8 m³/hr per kilogram controls humidity and stabilizes litter moisture around 18.2%, effectively mitigating floor egg contamination risks.
Q3: Why is automatic floor rearing system nest box design essential for commercial layer farms?
A3: Integrated nest boxes with belt speeds of 2.5 m/min ensure swift egg collection, reducing floor egg counts and preventing egg breakage losses in large-scale floor rearing systems.
Taiyu (HK) Group - One Of China Toppest Floor Rearing System Manufacturer
Taiyu (hk) group manufactures commercial floor rearing system machinery with automated 1,200 kg/hr chain feeders and 0.2 mpa high-precision drinker lines designed for industrial layer housing applications.
our global factory direct sales channel delivers durable poultry equipment directly from iso-certified production facilities to cut middleman costs for farm operators worldwide.
we provide comprehensive turn-key engineering solutions including floor layout design, equipment procurement, site installation, and operational training.
our experienced engineering team customizes complete layer floor housing systems to optimize indoor air exchange, bird stocking density, and feed conversion efficiency.
with robust manufacturing capabilities and international quality standards, taiyu supports commercial poultry enterprises across every stage of facility construction and expansion.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
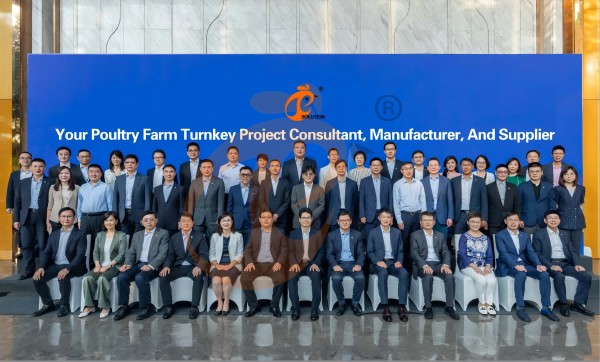
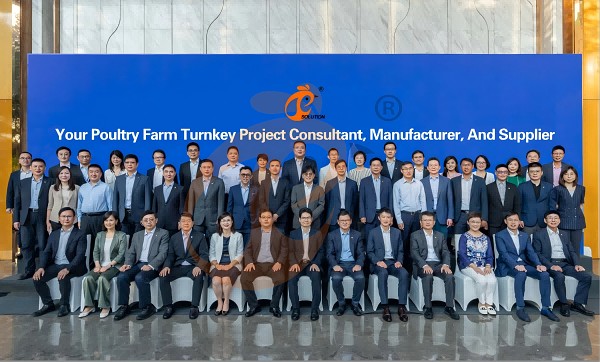
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
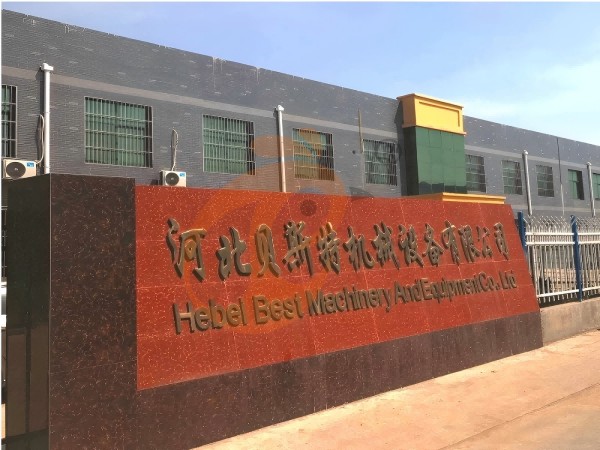
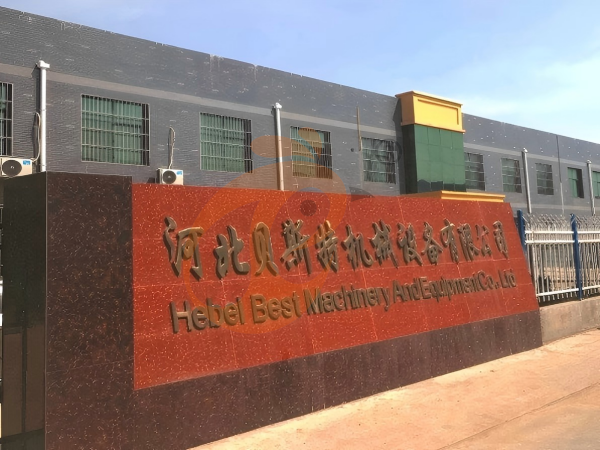
China Hebei Best Machinery And Equipment CO., LTD
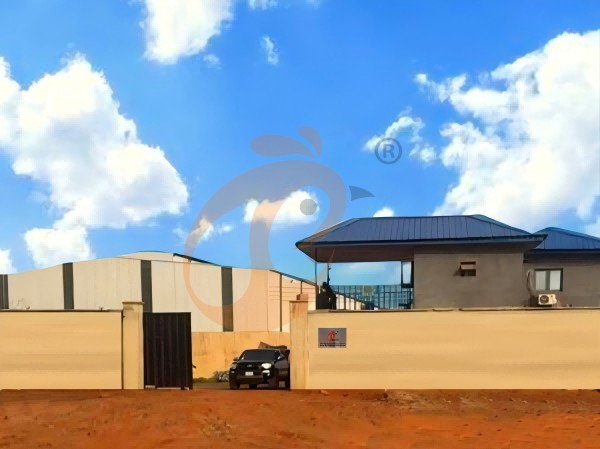
Nigeria Vanke Machinery And Equipment CO., LTD
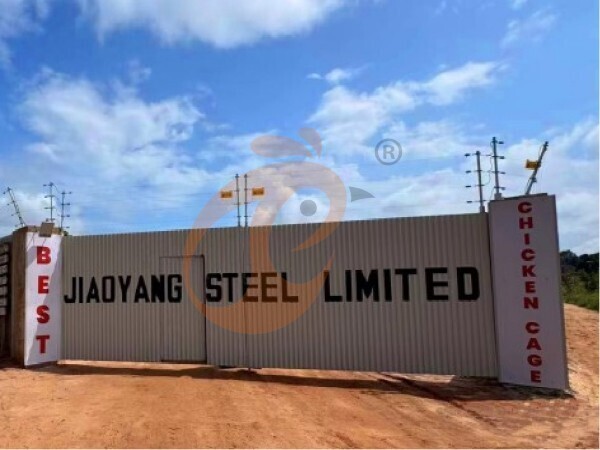
Tanzania Best Machinery And Equipment CO., LTD
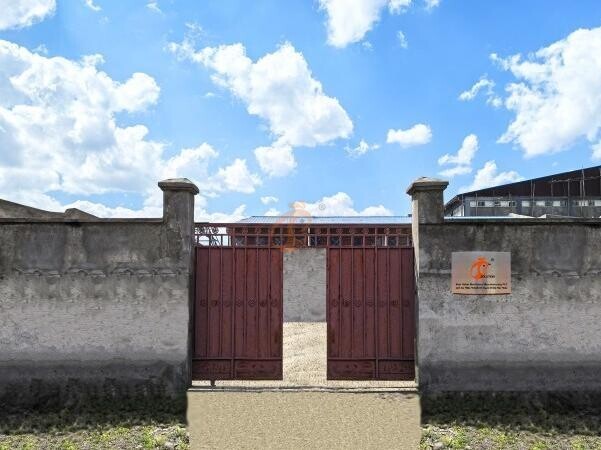
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
FAQ
What Growth Performance Indicators Are Expected In Floor Rearing Poultry System?
Feed conversion ratio is maintained at 1.65–1.85 for commercial broilers.
Market slaughter age ranges from 38–45 days depending on breed selection.
What Disease Control Standards Apply In Floor Rearing Poultry System?
Flock vaccination coverage reaches 90%–98% depending on disease prevention program.
Pathogen reduction targets aim for 80%–90% decrease in bacterial load.
What Are The Manure Management Requirements In Floor Rearing Poultry System?
Ammonia emission control targets remain below 15 ppm through regular cleaning cycles.
Dry matter content is maintained above 65% to improve composting efficiency.
Message
Products recommended
 HK Headquarter Offers EU-standard Poultry Farm Solutions, Manufacture Poultry Farm Equipment1. Continuous communication with the EU and the US
2. China, Nigeria, Ethiopia, Tanzania branch companies and factories
3. The products’ quality is customized for local poultry farms
4. Poultry cage and poultry farm equipment stock for sale
5. 24 online reception Whatsapp NO. : +8618830120193,contact us to get full informationRead More China Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province, China
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for local poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193Read More Nigeria Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: After Sinoma Office, 200 Meters Near Danco Filling Station, Lagos/Ibadan Expressway, Lagos State, Nigeria
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Nigerian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193Read More Ethiopia Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Gelan Gura, Akaki-kaliti Sub City, Addis Ababa, Ethiopia
2. Poultry cage and poultry farm equipment stock for sale
3. Customized for Ethiopian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193, contact us to get price listRead More Tanzania Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: No.8, Sova Road, Msufini, Mlandizi, Kibaha, Pwani, Tanzania
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Tanzanian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193Read More Fully Automatic H Type Layer Chicken Cage1. 30,000-100,000+ layers/house chooses it, Poultry farmers can achieve an egg production rate of 96-98%
2. A significant improvement over the 85-90% typically seen in manual systems
3. A typical poultry farm can expect a 30-40% reduction in labor costs due to the automation
4. Each feeding line efficiently supplies feed to around 100,000 hens per 30 mins
5. Reception /WhatsApp NO. : +8618830120193Read More Fully Automatic A Type Layer Chicken Cage1. 10,000-50,000 layers/house chooses it
2. Cleaner egg collection reduces breakage by 0.5%
3. Improved hygiene helps reduce mortality rate to <3%
4. 1–2 technicians can handle 15,000–30,000 birds
5. Reception /WhatsApp NO. : +8618830120193Read More Semi Automatic H Type Layer Chicken Cage1. 1,00-20,000 layers/house chooses it
2. Nipple drinkers flow 30–60 ML / min
3. Hot-dip galvanized (typical coating ≥ 275 g/m²)
4. Reduce ammonia by ~ 35–40%
5. Reception /WhatsApp NO. : +8618830120193Read More Semi Automatic A Type Layer Chicken Cage1. 1,00-20,000 layers/house chooses it, no rust for 10 years, no deformation for 15 years
2. Chickens live comfortably, you can raise them with peace of mind
3. Save water, save money—efficiency you can measure
4. Improve environment quality, and increase egg production rate
5. Reception /WhatsApp NO. : +8618830120193Read More
By clicking 'Allow All', you agree to the storage of cookies on your device to enhance site navigation, analyze site usage and assist with our marketing efforts.