


Blog
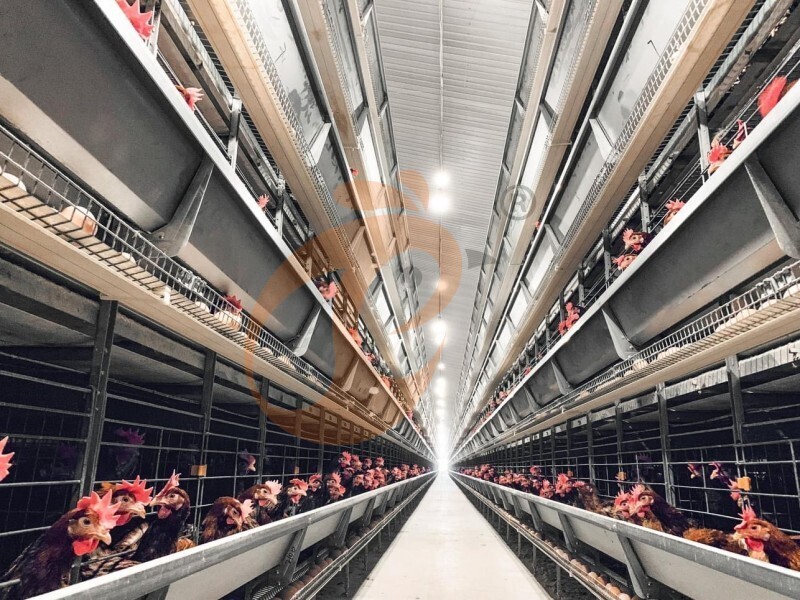
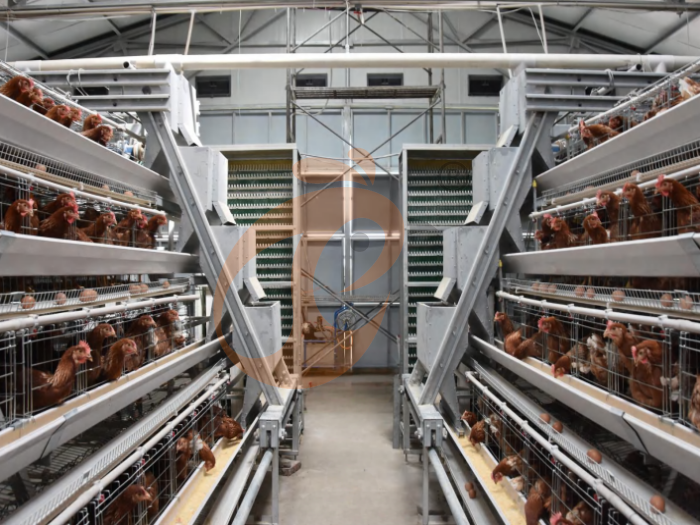
Broiler chicken cages integrate automatic feeding systems, ventilation, and manure handling for production, supporting 35–45 day cycles and 1.8–2.8 kg weights.
Cage geometry, galvanized steel, and tier arrangement influence structural stability, service life, airflow, and equipment integration across poultry houses.
Automatic broiler feeding systems coordinate delivery, while nipple drinking lines maintain water access through regulated pressure and stainless-steel components.
Automatic manure removal systems, cooling pads, lighting, and environmental controllers convert poultry-house operations into measurable production workflows.
Engineered broiler chicken cages improve space utilization, labor efficiency, equipment coordination, and expansion potential when systems match production targets.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, +2348111199996, or click to learn more.
Cage Density Starts With Engineering, Not Bird Numbers
Choosing broiler chicken cages should begin with the relationship between cage geometry, bird development, equipment configuration, and house conditions.
A commercial cage should be engineered around the target production cycle rather than simply increasing the number of birds inside each compartment, with daily feed consumption around 90–160 g/bird and market age commonly between 35–45 days.
For equipment manufacturers and commercial poultry producers, the real advantage comes from integrating broiler chicken cages with feeding, drinking, ventilation, cooling, and manure-management systems.
A correctly designed installation can maintain consistent production conditions across multiple tiers while reducing repetitive manual operations, while house aisle width of 1.0–1.5 m and service clearance of approximately 0.8–1.2 m support practical maintenance access.
Broiler Cage Engineering Parameters
Data is for reference only.Swipe horizontally to view full table.
Why Automated Feeding Matters As Capacity Increases
Feed distribution becomes a critical engineering issue when broiler chicken cages operate across several production tiers.
Manual feeding creates differences in delivery time and feed availability, whereas an automatic broiler feeding system can distribute feed through complete rows according to programmed schedules, supporting a feed conversion ratio of approximately 1.55–1.75 and 6–8 daily feeding events.
The feeder drive should also be selected according to line length, feed resistance, and total bird capacity rather than motor power alone.
For commercial broiler chicken cages, automated feeding can coordinate multiple circuits while maintaining feed-bin replenishment intervals of approximately 12–24 hours and feed wastage targets below 3%.
Automatic Feeding System Parameters
Data is for reference only.Swipe horizontally to view full table.
Drinking Equipment: Precision At Every Tier
Water delivery is another area where broiler chicken cages directly affect production consistency.
Nipple drinkers should be installed at carefully calculated positions so birds can reach drinking points without excessive movement within the cage, with daily water consumption commonly around 0.2–0.4 l/bird and water-to-feed ratios near 1.6–2.0:1 under moderate conditions.
The drinking system should include pressure regulators, water filters, main pipes, branch pipes, and flushing arrangements.
For commercial broiler chicken cages, proper water management can support drinking-line flushing every 1–3 days and maintain water temperature around 18–24°c where farm conditions allow.
Nipple Drinking System Parameters
Data is for reference only.Swipe horizontally to view full table.
Ventilation Is Where Cage Design Meets Climate Control
As bird numbers increase inside a poultry building, broiler chicken cages require ventilation equipment capable of removing metabolic heat, moisture, dust, and contaminated air without creating excessive drafts.
A tunnel ventilation strategy should account for house volume and seasonal conditions, while relative humidity can be maintained around 60–70% and carbon dioxide commonly controlled below 3,000 ppm as practical environmental targets.
Cooling equipment should operate as part of the same environmental-control strategy.
For broiler chicken cages, coordinated airflow can be supported by maintaining static pressure around 15–30 pa and keeping ammonia preferably below 10 ppm, depending on local standards and management conditions.
Environmental Control: Make Every Tier Part Of One System
An automated poultry-house controller can coordinate ventilation, cooling, lighting, feeding, and alarm functions around broiler chicken cages from one control interface.
Temperature sensors can be positioned at representative cage locations, while humidity sensors provide additional information for controlling moisture conditions, with temperature variation across occupied zones preferably within ±2°c and sensor calibration intervals around 6–12 months.
Alarm functions are equally important for automated facilities.
For large broiler chicken cages, power failure, abnormal temperature, water interruption, and ventilation faults can be monitored continuously, with backup generator capacity commonly sized at 80–100% of critical load and emergency inspection intervals around 15–30 minutes during abnormal events.
Ventilation And Cooling Equipment Parameters
Data is for reference only.Swipe horizontally to view full table.
Automatic Manure Removal Parameters
Data is for reference only.Swipe horizontally to view full table.
Automatic manure removal is particularly valuable for multi-tier broiler chicken cages because waste can be transported outside the bird area without requiring workers to repeatedly enter cage rows.
A properly scheduled manure-removal program can also reduce prolonged waste exposure, with removal intervals commonly set at 1–3 days and manure moisture often targeted around 25–35% for manageable handling.
Lighting And Electrical System Parameters
Data is for reference only.Swipe horizontally to view full table.
Lighting should be distributed uniformly across broiler chicken cages so each production zone receives consistent illumination.
A controlled lighting program can support approximately 16–20 hours of programmed light during selected production phases while maintaining 5–10 lux according to the management program and applicable welfare requirements.
Which Configuration Delivers Better Commercial Performance?
Data is for reference only.Swipe horizontally to view full table.
The comparison demonstrates why broiler chicken cages should be evaluated as a complete production system.
Increasing cage capacity without upgrading feeding, drinking, ventilation, manure removal, and environmental control can create bottlenecks, while target feed conversion ratios around 1.55–1.75 and mortality targets commonly below 5% provide useful commercial performance references.
Frequently Asked Questions
Q1: What factors determine whether broiler chicken cages perform efficiently?
A1: Broiler chicken cages perform efficiently when structural design, feed access, water supply, climate control, and manure handling are engineered as one system.
A practical evaluation can include feed conversion around 1.55–1.75 and mortality below 5% as management references.
Q2: Why is automatic feeding important for broiler chicken cages?
A2: Automatic feeding systems provide scheduled feed delivery and reduce repetitive manual work across long cage rows.
Commercial programs may use 6–8 feeding cycles per day according to bird age and feeding strategy.
Q3: How should ventilation be selected for broiler chicken cages?
A3: Ventilation should be calculated from bird load, building volume, climate, cage arrangement, and required airflow path rather than fan quantity alone.
Environmental planning can target carbon dioxide below 3,000 ppm and relative humidity around 60–70% under suitable operating conditions.
Taiyu (HK) Group - One Of China Toppest Broiler Chicken Cages Manufacturer
Broiler chicken cages provide integrated galvanized steel housing with automated feeding, drinking, manure removal, and climate-control interfaces for commercial poultry projects.
Global factory-direct production covers poultry equipment with configurable cage layouts, electrical systems, automation packages, and project-specific engineering documentation.
Turn-key engineering combines equipment manufacturing, system integration, installation guidance, commissioning support, and production-oriented technical coordination.
International project delivery supports complete poultry equipment packages for farms requiring scalable capacity, coordinated utilities, and standardized installation procedures.
Engineering teams develop broiler chicken cages according to house drawings, bird specifications, equipment loads, environmental requirements, and long-term maintenance considerations.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
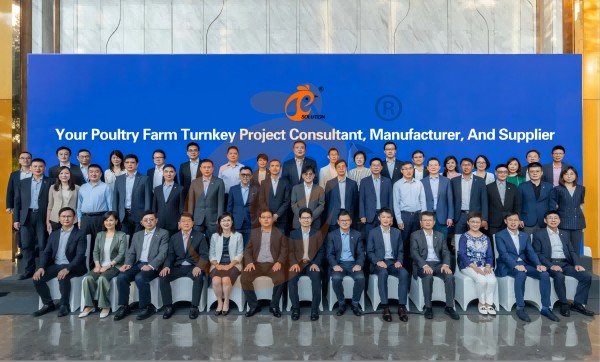
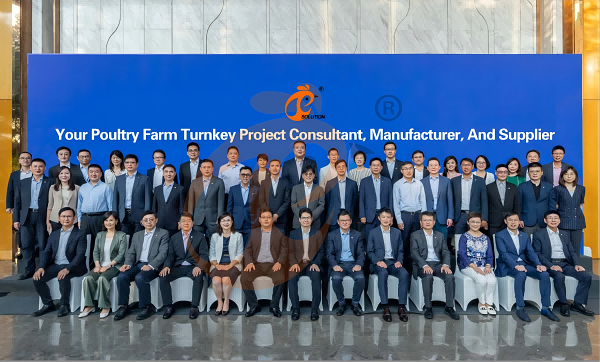
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
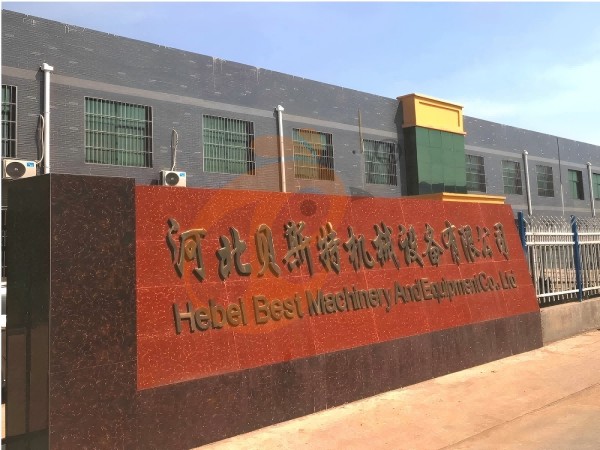
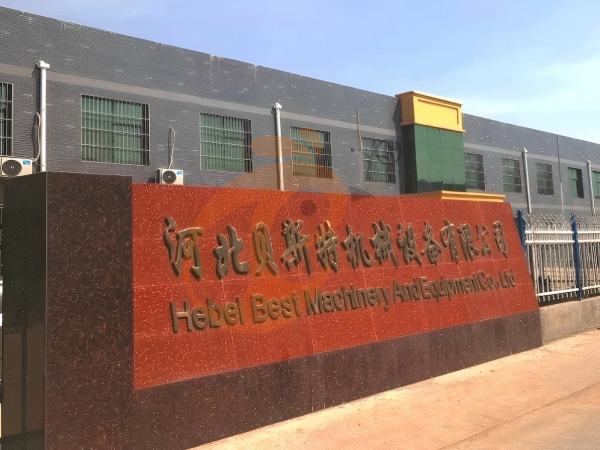
China Hebei Best Machinery And Equipment CO., LTD
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
FAQ
What Cage Structure Options Are Available For Broiler Chicken Cage Systems?
H-type cage systems are configured in 3–12 tiers accommodating 360–1440 birds per set for intensive farming operations.
Structural height ranges from 1.75–10.11 meters maximizing vertical space utilization and housing efficiency.
How Does Stocking Density Affect Broiler Chicken Cage Performance?
H-type systems maintain 500 cm² allocation per bird optimizing housing density and production output.
Bird distribution is balanced at 8 birds per compartment in partitioned cage configurations reducing competition.
Which Cage Dimensions Are Commonly Used In Broiler Chicken Cage Systems?
H-type cage modules measure 3.3 × 1.82 meters providing larger continuous housing sections.
Internal compartment height varies from 40–55 cm ensuring adequate bird activity and ventilation circulation.
Message
Products recommended
 HK Headquarter Offers EU-standard Poultry Farm Solutions, Manufacture Poultry Farm Equipment1. Continuous communication with the EU and the US
2. China, Nigeria, Ethiopia, Tanzania branch companies and factories
3. The products’ quality is customized for local poultry farms
4. Poultry cage and poultry farm equipment stock for sale
5. 24 online reception Whatsapp NO. : +8618830120193,contact us to get full informationRead More China Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province, China
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for local poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193Read More Nigeria Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: After Sinoma Office, 200 Meters Near Danco Filling Station, Lagos/Ibadan Expressway, Lagos State, Nigeria
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Nigerian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193Read More Ethiopia Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Gelan Gura, Akaki-kaliti Sub City, Addis Ababa, Ethiopia
2. Poultry cage and poultry farm equipment stock for sale
3. Customized for Ethiopian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193, contact us to get price listRead More Tanzania Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: No.8, Sova Road, Msufini, Mlandizi, Kibaha, Pwani, Tanzania
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Tanzanian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193Read More Fully Automatic H Type Layer Chicken Cage1. 30,000-100,000+ layers/house chooses it, Poultry farmers can achieve an egg production rate of 96-98%
2. A significant improvement over the 85-90% typically seen in manual systems
3. A typical poultry farm can expect a 30-40% reduction in labor costs due to the automation
4. Each feeding line efficiently supplies feed to around 100,000 hens per 30 mins
5. Reception /WhatsApp NO. : +8618830120193Read More Fully Automatic A Type Layer Chicken Cage1. 10,000-50,000 layers/house chooses it
2. Cleaner egg collection reduces breakage by 0.5%
3. Improved hygiene helps reduce mortality rate to <3%
4. 1–2 technicians can handle 15,000–30,000 birds
5. Reception /WhatsApp NO. : +8618830120193Read More Semi Automatic H Type Layer Chicken Cage1. 1,00-20,000 layers/house chooses it
2. Nipple drinkers flow 30–60 ML / min
3. Hot-dip galvanized (typical coating ≥ 275 g/m²)
4. Reduce ammonia by ~ 35–40%
5. Reception /WhatsApp NO. : +8618830120193Read More Semi Automatic A Type Layer Chicken Cage1. 1,00-20,000 layers/house chooses it, no rust for 10 years, no deformation for 15 years
2. Chickens live comfortably, you can raise them with peace of mind
3. Save water, save money—efficiency you can measure
4. Improve environment quality, and increase egg production rate
5. Reception /WhatsApp NO. : +8618830120193Read More
By clicking 'Allow All', you agree to the storage of cookies on your device to enhance site navigation, analyze site usage and assist with our marketing efforts.